MOSQITO machine park
The MOSQITO machine park lets us fabricate and produce metal parts in one place. We use a MAZAK Super Turbo MK II laser for sheet cutting, a TRUMPF C60 press brake for CNC bending, a Tauring Delta CNC for tube and profile rolling, laser welding, MIG/TIG and a Universal Robots robot. The process is completed by spot welding, laser marking, 3D CAD design and precision finishing.
Specialist processes, our own machines and production experience let us make parts to technical documentation — from design to a finished component.
Laser cutting
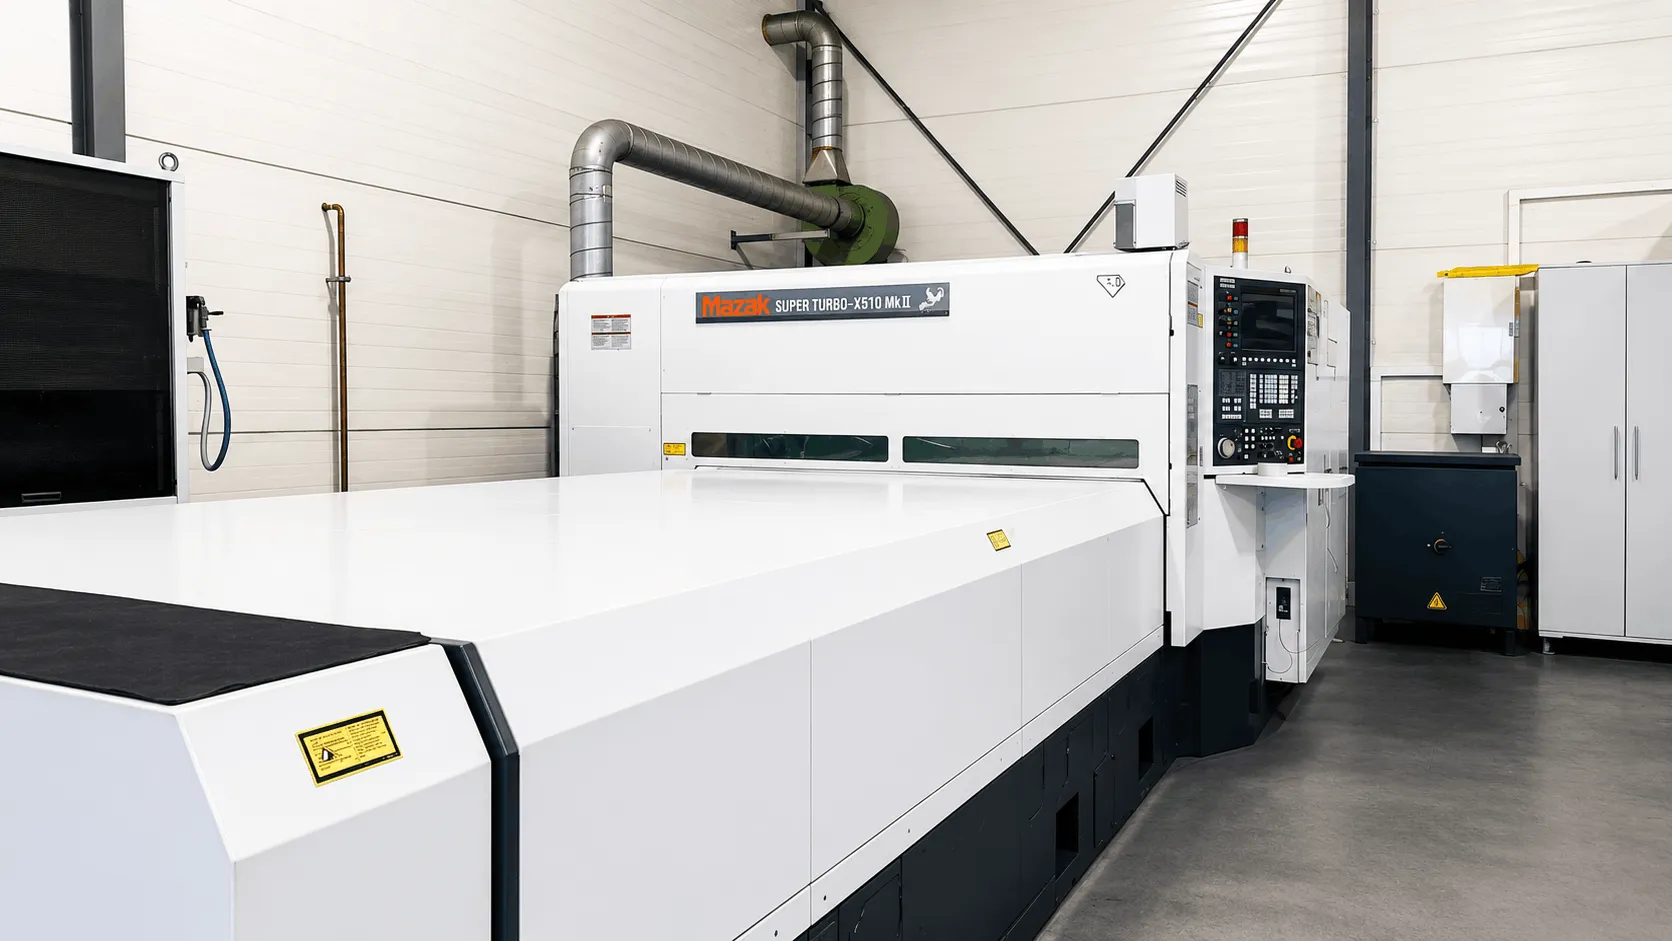
MAZAK Super Turbo-X510 Mk II · 3000 × 1500 mm
Cutting of mild steel, stainless steel and aluminium sheet on a 2D laser. The 3000 × 1500 mm working format prepares parts from DXF and DWG documentation with a repeatable edge. We use it where hole, nest and outline accuracy matters before bending or welding.
CNC sheet metal bending
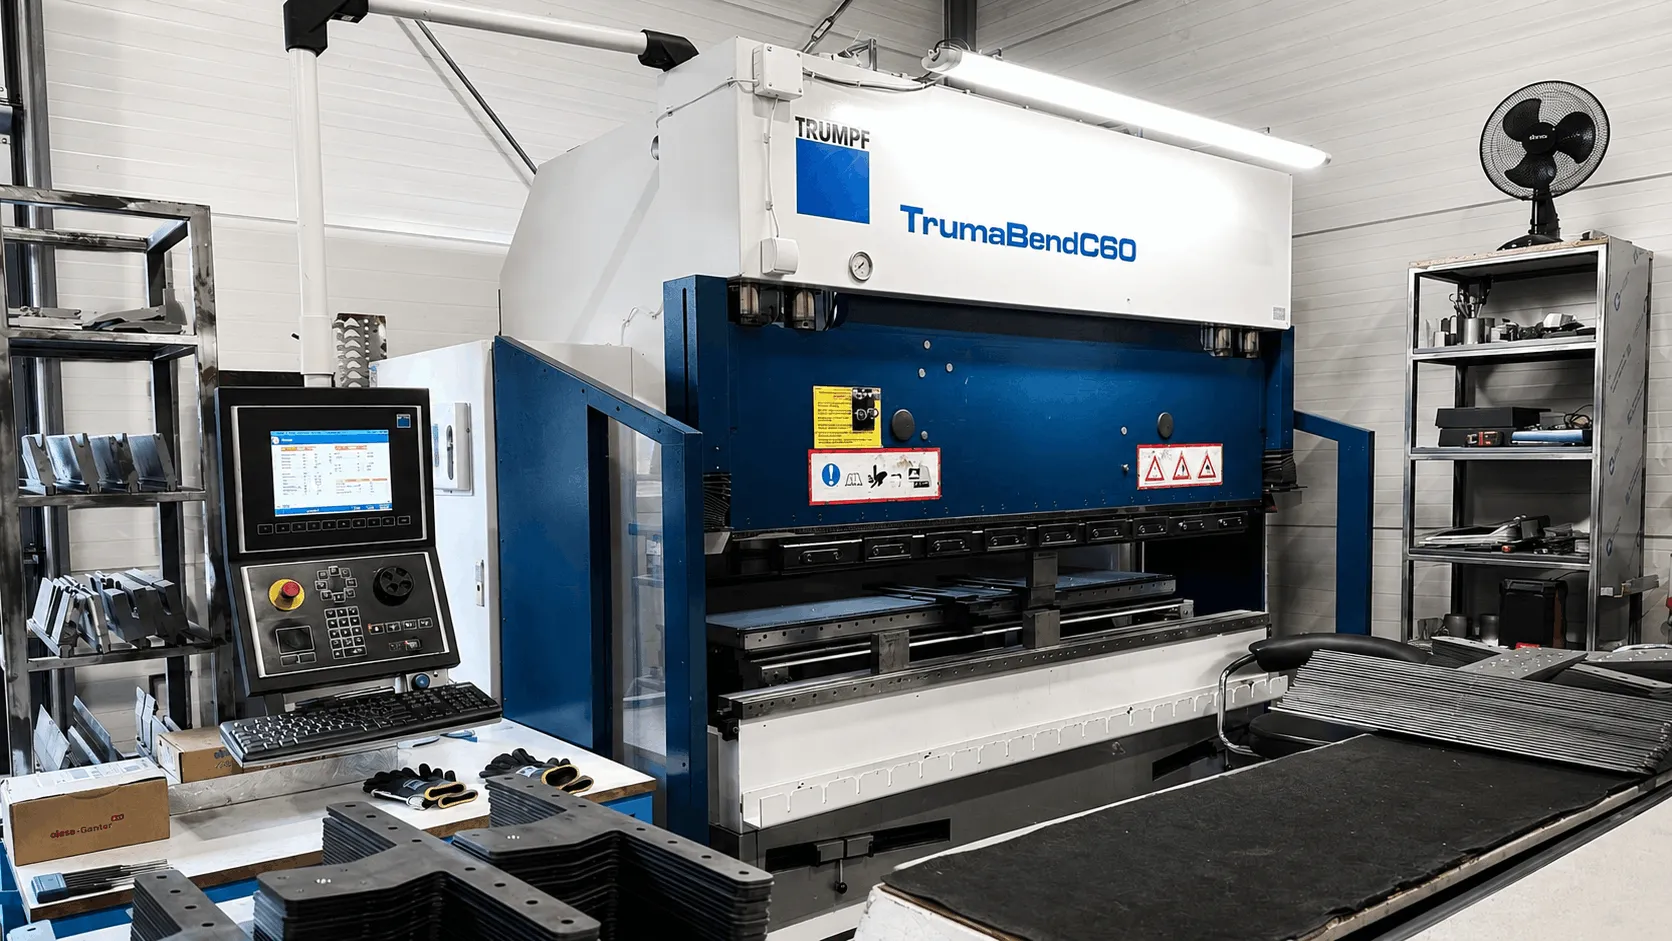
TRUMPF C60 · up to 220 t · bending length 3000 mm
CNC sheet bending on a TRUMPF C60 press brake. Force up to 220 tonnes and a 3000 mm bending length suit housings, brackets and structural parts. The CNC programme keeps angles and bend sequence to the drawing, including larger series.
Tube and profile rolling
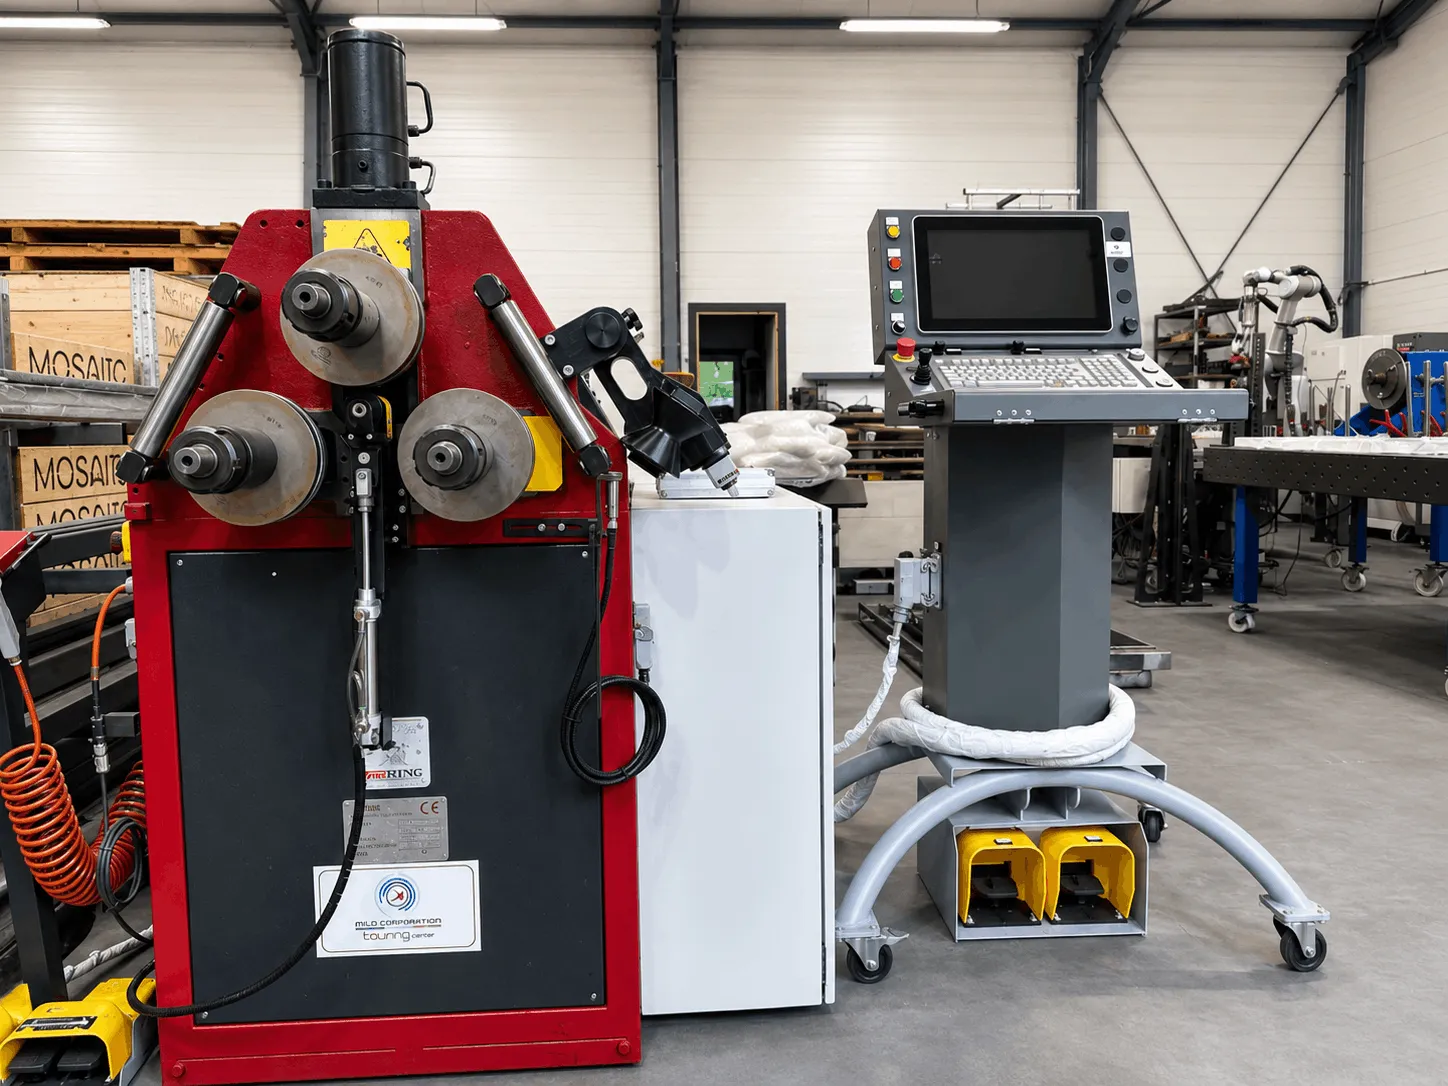
Tauring Delta CNC
Rolling of tubes, hollow sections and special profiles. On the Tauring Delta CNC we make arcs, circles, ellipses and spirals to a set radius. We can assess the job from a drawing, a profile cross-section or a 3D model.
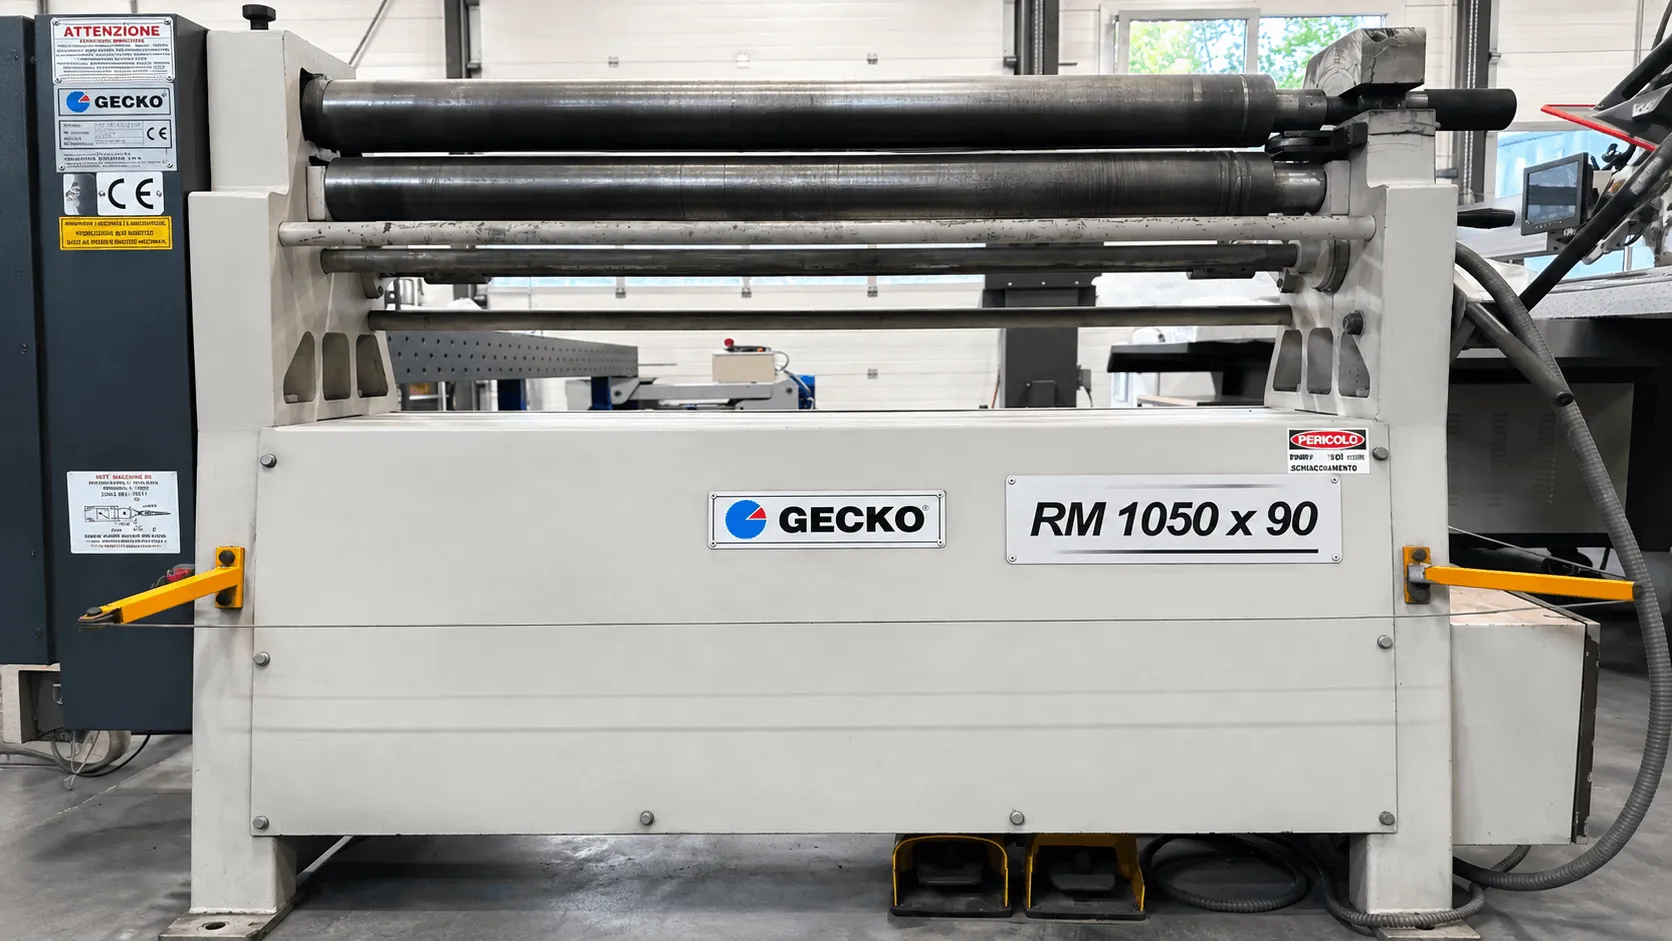
Sheet metal rolling
GECKO RM 1050 × 90 · width 1050 mm · thickness up to 3 mm
Sheet rolling on a machine with a working width of up to 1000 mm and material thickness up to 3 mm. We form flat sheets into cylindrical and curved parts when the documentation calls for roll forming instead of press-brake bending.
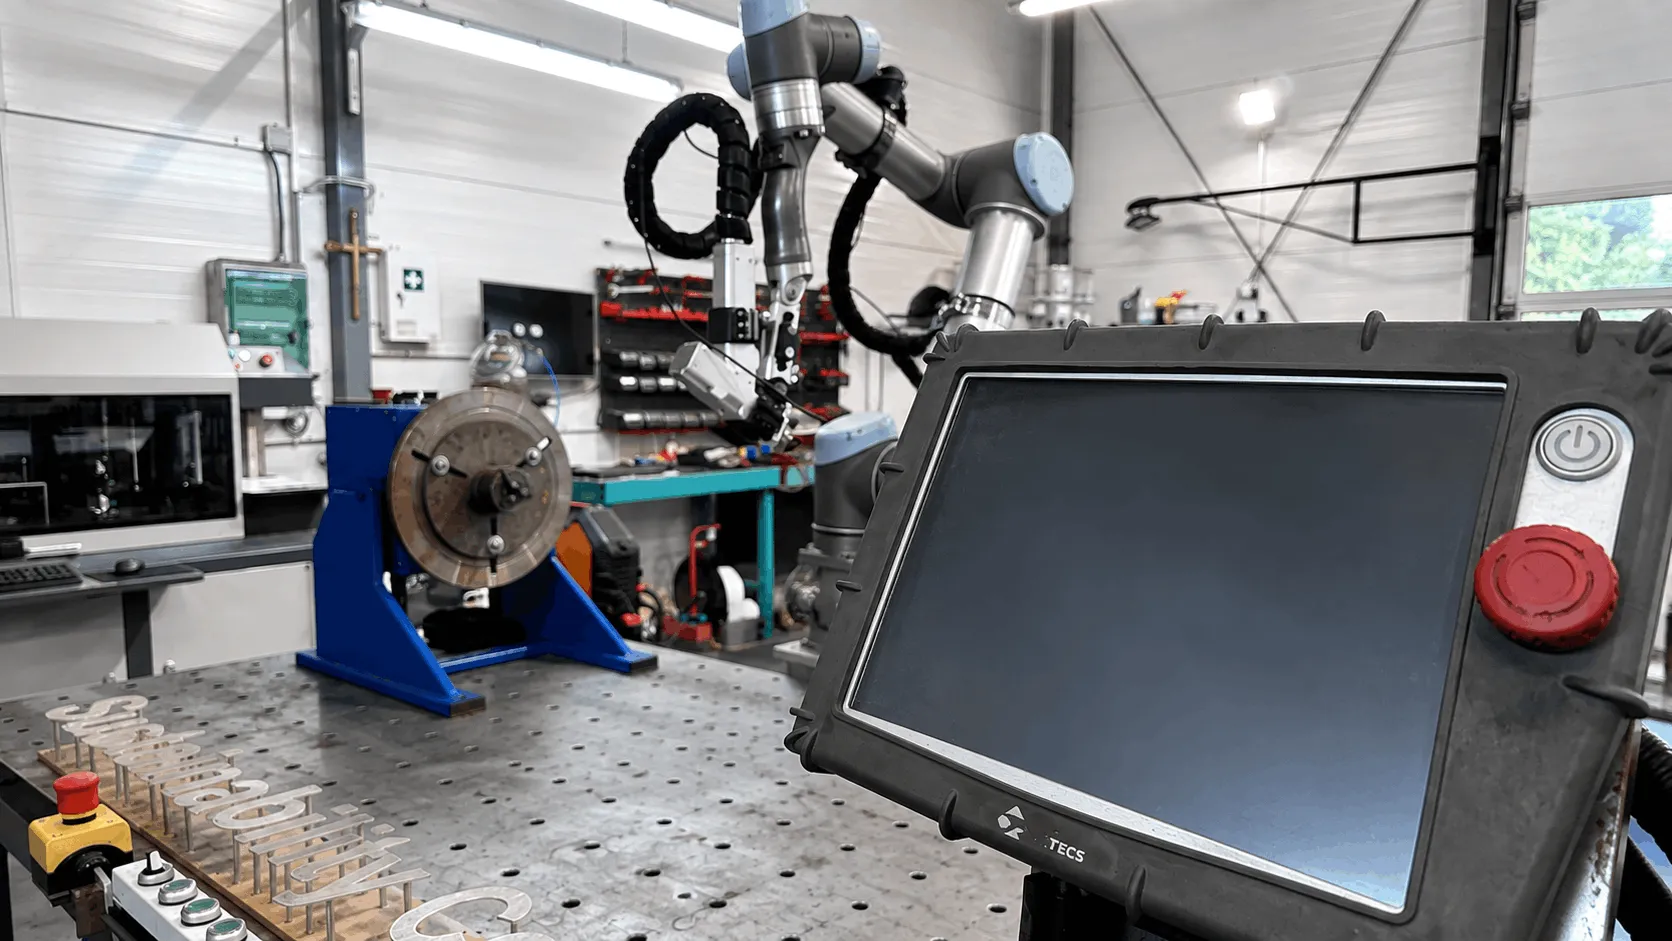
Robotic laser welding
Universal Robots · laser welding
Laser welding with a Universal Robots robot. A narrow weld, low heat input and limited sheet distortion. Suited to repeat joints where weld appearance and dimensional stability matter after joining several parts.
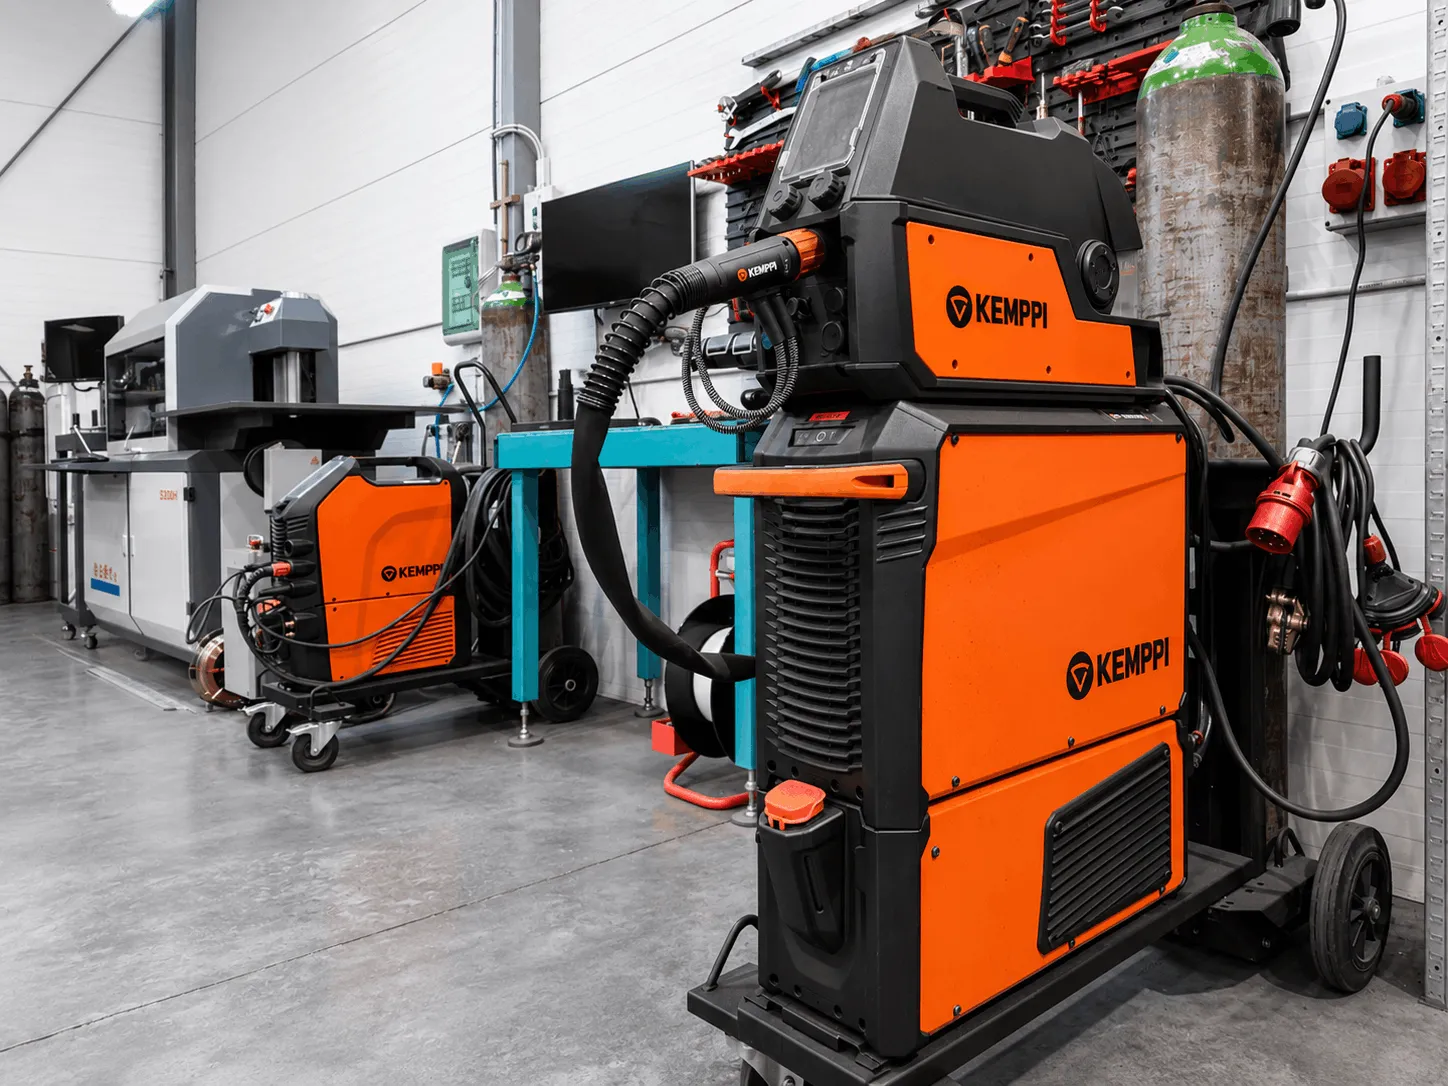
MIG / TIG welding
MIG / MAG · TIG · laser
Manual and semi-automatic MIG/MAG and TIG welding complements the laser station. We choose the method for the material grade, thickness and access to the weld. We join structural steel, stainless steel and aluminium when the project needs a load-bearing or a visual weld.

3D letter production
S200
Automatic bending of strip and profiles on an S200 bender. We prepare repeat outlines from documentation when the project needs bending of narrow material instead of a press brake.

Spot welding of sheet metal
ASPA
Spot welding of sheet metal on an ASPA welder. We assess each job from the material, thickness, geometry and documentation.
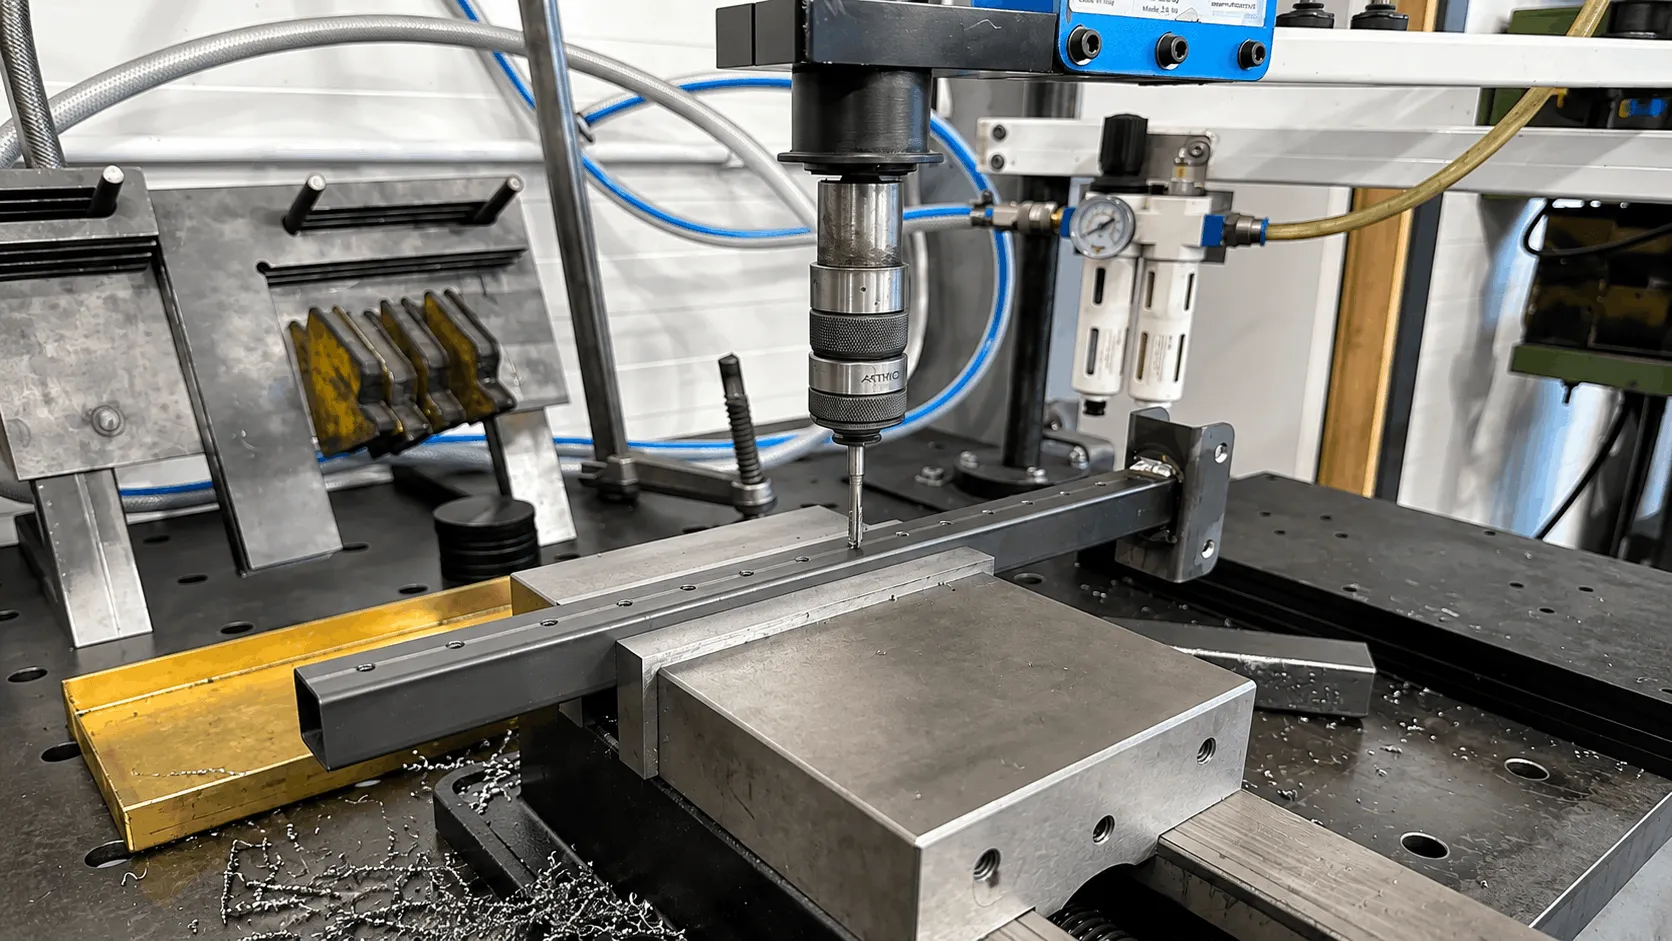
Finishing
grinding · satin finishing · deburring
Grinding, satin finishing and edge deburring after cutting and welding. We remove burrs, dress welds and prepare the surface for assembly, painting or further work. The finish is agreed at quoting so we do not promise a process the documentation does not require.